
Case Study
Large-Scale Mammalian Biologics Facility — Full DeltaV & Syncade Build, Kneat eValidation System and 24/7 CQV Support Through PPQ
The Challenge
One of the largest single CDMO facility investments in European biologics manufacturing history.
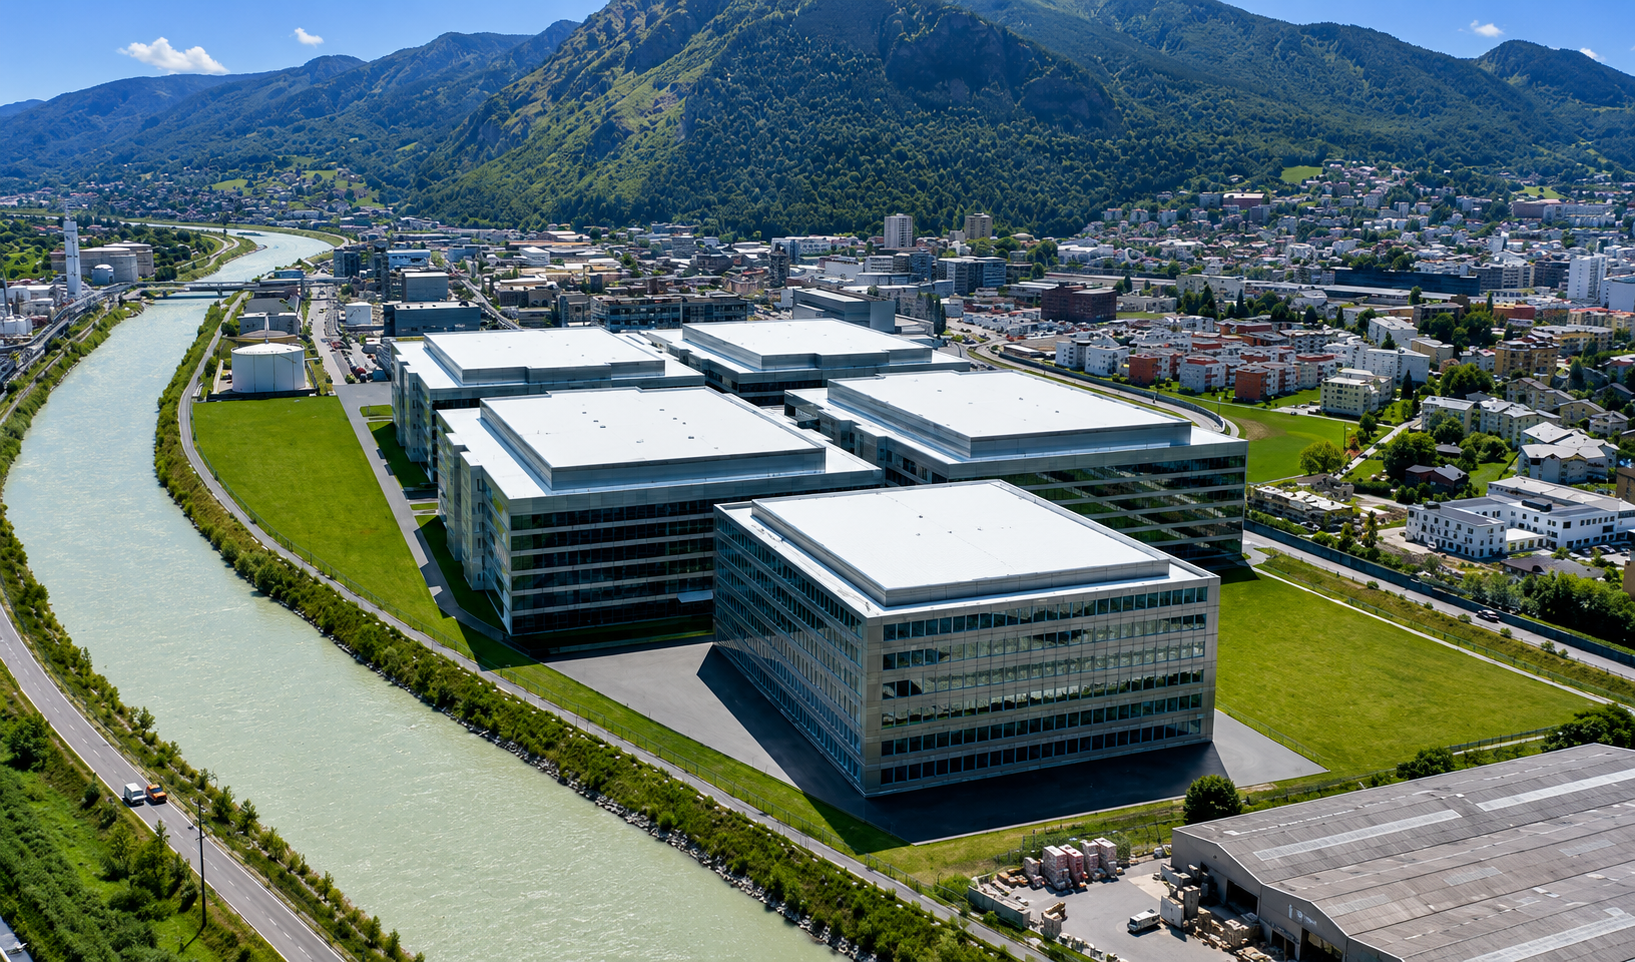
One of the world’s leading CDMOs was constructing a major new large-scale mammalian drug substance manufacturing facility in southern Switzerland — a state-of-the-art biologics plant built around six 20,000 litre bioreactors across 27,500 square metres, representing a CHF 650 million investment, designed to support high-titer processes, perfusion capabilities and the next generation of commercial mammalian biologics. One of the largest single CDMO facility investments in European biologics manufacturing history.
The automation, eValidation and CQV scope was unlike anything a standard engineering programme encounters. Six 20,000 litre production bioreactors with full upstream seed train, a complete downstream processing train — capture chromatography, viral inactivation, HIC, CEX, AEX polishing, viral filtration, UF/TFF — CIP/SIP across every piece of process equipment, USP utilities (WFI, purified water, clean steam), HVAC and a BMS across 27,500 square metres. Every system needed DeltaV configured from the recipe layer, Syncade implemented across the full process scope, and a complete eValidation system built from scratch on Kneat.
The delivery model added the final dimension: 24/7 engineering presence through the full qualification lifecycle — multiple engineering batches, validation batches and PPQ — with Rockstone’s Process Automation Engineers on site continuously from commissioning through to PPQ and regulatory submission readiness.
The Scope
-
DeltaV DCS — full facility build from the recipe layer
Emerson DeltaV was configured across the complete facility scope from the ground up — upstream seed train, six 20,000 litre production bioreactors (fed-batch and perfusion), harvest and centrifugation, full downstream processing train, CIP/SIP, USP utilities and BMS integration. Every system was built from the recipe layer — ISA-88 phase logic designed around the specific equipment and process requirements for each area, not generic modules from a template. The DeltaV architecture was consistent and standardised across the entire 27,500 square metre facility — same control philosophy, same alarm management framework, same data structure throughout.
-
Syncade MES — full facility implementation
Emerson Syncade was configured across the entire facility scope — recipe management for all upstream and downstream process steps, electronic batch records from seed train through to DS formulation, weigh and dispense module for raw material management, and full DeltaV-Syncade integration so every DCS-controlled process event was automatically captured in the correct Syncade batch record in real time. The implementation covered CIP/SIP cycle records, utility system records and every in-process step — so the electronic batch record produced at completion of every batch was genuinely complete and automatically structured for QA review.
-
Kneat eValidation system — built from scratch
Rockstone built the facility’s complete eValidation system on Kneat — the leading digital validation platform chosen by 12 of the world’s top 15 pharmaceutical companies. Designed and built from the ground up for this facility and scope: the overall computer system validation plan, recipe testing plan, design document templates, testing document templates (IQ, OQ, PQ protocols) for all process equipment, utilities and computerised systems, and the change control framework governing every modification through the qualification programme. Every qualification protocol, testing record and change control ran through the Kneat platform — creating a single, structured, electronically traceable validation record for the entire facility.
-
24/7 CQV support — engineering batches through PPQ
Through commissioning and qualification — engineering batches, validation batches and PPQ — Rockstone’s Process Automation Engineers provided 24/7 on-site support. When a 20,000 litre bioreactor ran at 03:00, a Rockstone engineer was there. When a CIP sequence generated an unexpected deviation on the night shift, a Rockstone engineer resolved it in real time, managed the change control in Kneat and documented the impact assessment before the next shift started. The 24/7 model was a delivery requirement — PPQ batches are the batches that go into the regulatory submission, and having the engineers who built the system present throughout was the difference between a qualification programme that ran on schedule and one that accumulated findings and delays.
The Outcome
- ~3,000 recipe objects configured across the facility
- 6,500+ qualification documents executed in Kneat
- 6 20,000L bioreactors qualified through PPQ
The PPQ batches were executed on a DCS and MES platform that Rockstone’s engineers had built from the recipe layer and were present to support in real time throughout. Every Syncade electronic batch record was complete at the point of batch completion — automatically generated, fully traceable and structured for regulatory submission without manual compilation. The Kneat eValidation system became the facility’s validated qualification baseline — the framework every subsequent change control, modification and requalification at the facility references.